


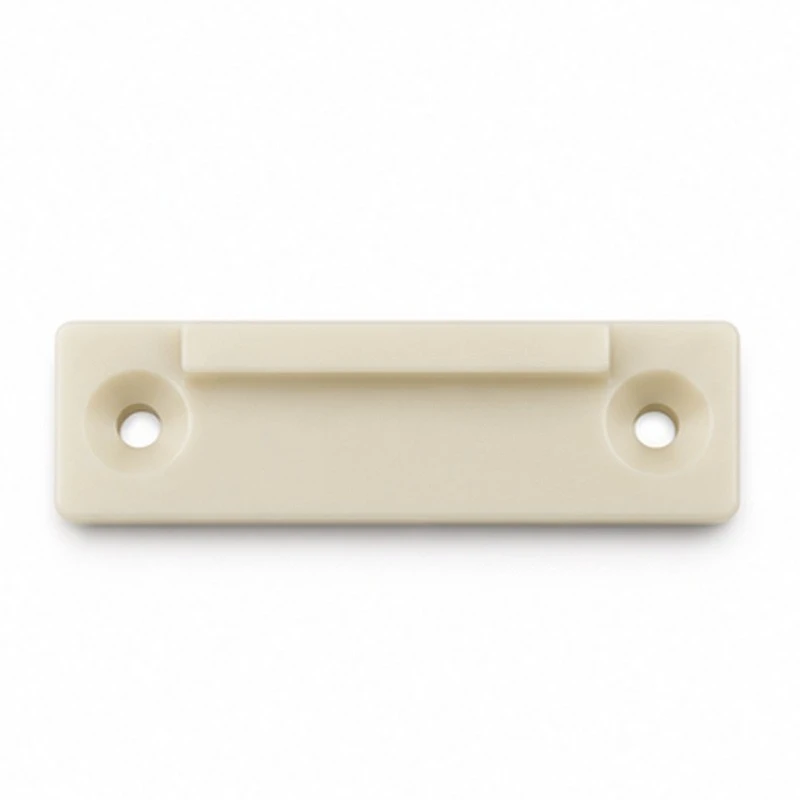


Tianjin SWKS Technology & Development Co.,Ltd is one of the most reliable manufacturers and suppliers of custom pom industrial packaging machine sealing jaw insert in China. If you're going to buy bulk cheap custom pom industrial packaging machine sealing jaw insert, welcome to get quotation from our factory. Quality products and low price are available.
Custom POM Industrial Packaging Machine Sealing Jaw Insert
This POM part is a locator or support behind a packaging jaw. Use is on the thermally separated side of the assembly, subject to measured part temperatures and grade approval. The heater, film-contact face and product-contact equipment are specified separately. Pictures are generated examples for project discussion. All finished dimensions, material specification and qualification requirements depend on the approved design.
Identify the cold-side locator before describing the assembly
This product description covers a POM insert positioned behind a packaging machine sealing jaw. The heat-producing element, the hot jaw face and the region that handles film are defined separately. Use a section view showing the actual thermal path and the location of the molding. A name such as jaw insert can describe several different parts on a line: a hot contact tool, an insulated backup plate or a holder that indexes a change part. Each role changes which materials and checks the equipment designer must consider.
Product specification
| Material | POM |
| Manufacturing method | Custom injection molding |
| Application | packaging machinery jaw assemblies |
| Assembly references | metal jaw carrier, insulated support, locating screws and replaceable sealing face |
| Drawing formats | STP, STEP, IGS and a dimensioned print |
| Validation scope | seating on the cold side, clearance during jaw motion, changeover repeatability and OEM qualification of the installed arrangement |
At sample approval, document the physical separation from the jaw face and temperature at the intended polymer location. The part manufacturer and the purchaser can then review the same configuration. Retain the reference setup, including the way the component is supported and the selected mating items. A difference between an unmounted measurement and an assembled one should be documented with the condition and measuring point. This avoids deciding whether a sample is usable based only on the shape visible in a photograph of cold-side sealing-jaw locating insert.
Establish the occupied space through the jaw cycle
Share a drawing or model with the jaw open and closed at the approved positions. Record the nearest metal part, film path and any shield or heat break. During a film change, the jaw may open beyond its normal sequence, and the space needed to remove the insert can differ from its operating envelope. Show the approved removal direction and explain whether the part is inserted before or after the separate sealing surface. Dimension the mounting ledge relative to the metal carrier instead of placing all inspection points on the visible outline.

Use a controlled sample to define the path and limits of the film and how it clears the insert. Before agreeing on a manufacturing tolerance, identify which areas can use ordinary process variation and which need a specifically documented result. The priority should be the features related to installation, the agreed service role and the checks in the equipment drawing. Label the revision of the molding and mating components if any decision is made during a pilot run for packaging machinery jaw assemblies.
Check the stand-off from the hot assembly
The actual temperature where the plastic would sit is the relevant material input. The heater setpoint alone cannot establish that temperature. Provide measured or equipment-owner-approved conditions for steady running, warm-up and the period following shutdown, along with the grade requirement for the proposed molded insert. A cold-side component can still sit next to a heat source when an adjacent bracket changes. Review the thermal stack with the machine designer before approval. The image illustrates a possible locator and does not suggest POM for a film-contacting hot face.
On the quotation review, identify the ledge or mounting pocket that establishes the insert position. Add an acceptance method to the drawing when the requirement cannot be understood from the model alone. Explain whether the initial check requires a fixture, a reference assembly or a representative installed component. If an inspection report is requested, agree on the fields that must appear in the report before ordering pilot parts. This helps keep the assessment of cold-side sealing-jaw locating insert separate from qualification of the complete equipment.
Decide what carries the sealing force
Trace the reaction from the metal jaw through the tool and supporting equipment. Specify whether the POM molding is only a position aid or carries any limited load in the approved design. A screw can retain an insert without directing the jaw force into the insert. Mark the shoulders and stops that control the installed position and identify any separately sourced washers. If two inserts are used for left and right positions, annotate the side and direction in the assembly model so the first articles are inspected in the correct pockets.

During a review of cold-side sealing-jaw locating insert, ask the owner to show screw heads, access tools and the backing plate. Treat this as a controlled interface rather than an appearance preference. A model supplied alone may have enough information for a rough quotation while omitting the references needed to confirm assembly. For an engineering review of packaging machinery jaw assemblies, mark the relevant surfaces on both the customer assembly and the part drawing. Indicate which dimensions are checked before assembly and which depend on the selected mating items.
Plan a real format changeover trial
Record the packaging format and the part number of the jaw assembly in the test. Check that the operator can access screws without contacting nearby film guides or cables. Observe the positioning condition after the insert has been removed and reinstalled using the approved sequence. If the feature establishes a repeatable position for another component, include that component in the trial and record its installed reference. Do not infer sealing strength from a plastic locator fit check. Seal acceptance belongs to trials of the complete packaging process and the specified film.
Ask the design team to record whether the operator changes inserts with each printed-film format or during maintenance. A useful review separates the manufactured component from the extra space needed to install it. Record the position and any access requirement after nearby hardware is fitted. When different equipment revisions share an outer shape, include a separate view of each arrangement. This gives purchasing a clear way to trace a request for cold-side sealing-jaw locating insert to the assembly that actually needs it.
Record cleaners and press consumables
Include the shop cleaner, debris the operator removes at changeover, any local lubricant and the accepted appearance of the exposed face. Specify both the operating and cleaning conditions where they differ. A minor change in edge relief can help fit if it stays clear of the working film path and does not remove material in a critical seating area. Separate mold comments from application decisions so an accepted tooling change is evaluated on the current jaw assembly.
For this item the drawing package should give the complete context. Specifically, find out whether warm and cold equipment positions change the clearances. The best section is one that shows the feature in its intended assembled state. Include hardware type and any permitted alternate part. If access or fit changes with the alternate, quote an agreed revision first and review the second configuration before sharing a tooling decision. Keep the part data for packaging machinery jaw assemblies tied to its intended revision.
Purchase and sample approval
Each change request should identify the mating part and the feature affected. If a drawing is converted from a previous assembly, give the new revision and note the locating method. Agree how accepted samples and records will be labeled and retained. Include color, shipment quantities and documentation requirements when requesting a quotation so that ordering information stays associated with the correct design.
Place the sample order against a dated engineering baseline. A quotation issued before the mating assembly is fixed can state assumptions for the areas still open. Label each proposed change to the plastic geometry and ask the owner to accept it against the latest assembly view. If more than one cavity is planned, explain whether dimensional results must identify each cavity. Send an estimated production range so the tooling plan reflects the likely supply requirements.
Cold position in the project record
During a review of cold-side sealing-jaw locating insert, ask the owner to find out whether warm and cold equipment positions change the clearances. Treat this as a controlled interface rather than an appearance preference. A model supplied alone may have enough information for a rough quotation while omitting the references needed to confirm assembly. For an engineering review of packaging machinery jaw assemblies, mark the relevant surfaces on both the customer assembly and the part drawing. Indicate which dimensions are checked before assembly and which depend on the selected mating items.
Thermal separation in the project record
Ask the design team to document the physical separation from the jaw face and temperature at the intended polymer location. A useful review separates the manufactured component from the extra space needed to install it. Record the position and any access requirement after nearby hardware is fitted. When different equipment revisions share an outer shape, include a separate view of each arrangement. This gives purchasing a clear way to trace a request for cold-side sealing-jaw locating insert to the assembly that actually needs it.
Related SWKS products include Custom POM Industrial Packaging Machine Timing Belt Tensioner and Custom POM Industrial Packaging Machine Folding Guide Finger.
For a drawing-based quotation, send the assembly references and required quantity to amanda@tjswks.com.
Hot Tags: custom pom industrial packaging machine sealing jaw insert, China, suppliers, manufacturers, factory, bulk, cheap, low price, quotation, ABS machine parts, PA6 PA66 Nylon Parts quotation, polypropylene plastic, Polyurethane Coated Wheels And Rollers, Polyurethane PU Coated Wheel Roller, Soft Tooling Injection Molding


